

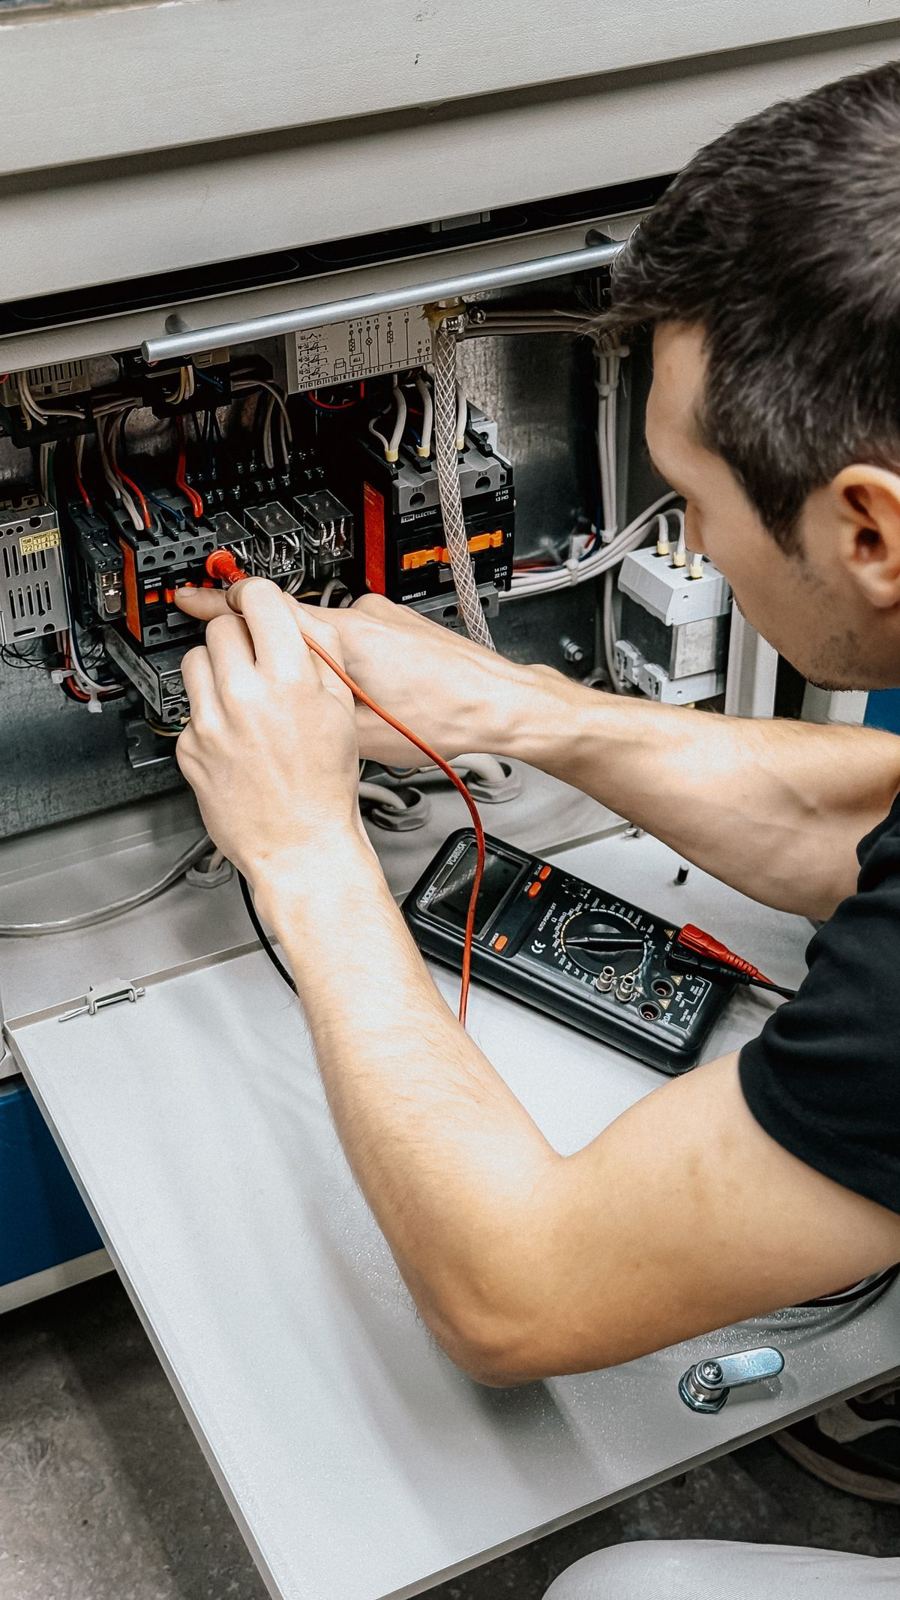
Maintenance work with lockout enforced and every reading kept.
Vexum runs your preventive and breakdown procedures step by step, requires the lockout steps and keeps every reading on the record with the machine it belongs to.
Maintenance procedures, worked step by step.
Preventive maintenanceBreakdown repairLockout and tagoutSpindle serviceCalibrationLubrication routesEquipment start-up
Work it
Lockout first. Then the work.
The lockout step is required, so nobody reaches the service steps without it. Vexum pulls the machine’s history and compares each reading to its limit.
- Required steps can’t be skipped
- Readings compared to limits as they’re entered
- The work order drafted for a person to close
Spindle serviceMill 4 · due today, 12:00
In progress- Apply lockoutRequired · M. Ito, 09:04Operator
- Pull machine history3 prior work ordersAutomated
- Measure runout0.004 mmOperator
- Compare to limitWithin 0.005 mmAutomated
- 5Adjust or replaceWaiting for M. ItoAssisted
- 6Close work orderDrafted for sign-offDrafted
Lockout recorded before any service step opened.
Ask
Answers from your manuals, history and systems.
Ask whether this has happened on this machine before and get an answer with its sources: past work orders, the maintenance log and the page of the manual.
- Every answer cited
- Gaps flagged, never guessed
- Asked from inside the step you’re on
Spindle serviceStep 5 · Adjust or replace
LiveHas Mill 4 had runout problems before?
Twice this year. In March the spindle bearing was replaced after runout reached 0.009 mm. In June runout was 0.006 mm after a tool crash and was corrected by re-seating the tool holder.
Work order 1184Work order 1302Maintenance logSpindle manual, p.42
Train on it
What your best technician knows, built into training.
Training is built from the procedure and from how your experienced people actually did the job, then assigned by role, shift or location.
- Built from real work orders
- Worked step by step on a past case
- Completion tracked for every version
Spindle service trainingReal case from March · 2 of 4
Measured0.009 mm
Limit0.005 mm
What do you do next?
Re-seat the tool holder and measure again.
Keep running and check at the next PM.
Lock out and inspect the spindle bearing.
Right. Above 0.008 mm the procedure calls for a bearing inspection.
Using a tool like this to recognize tribal knowledge is a much better approach than asking people to stop relying on it.
One platform for every procedure.
 ProceduresYour documents, turned into step-by-step procedures with every step cited.
 WorkspaceWhere your team works each procedure, with the routine steps done in your systems.
 Change managementEvery change proposed, approved and published, with the full history.
 TrainingBuilt from your procedures and real cases, then assigned and tracked.
 IntegrationsCustom-built for every system you use, read-only by default.
Built for every team that works from procedures.
 QualityComplaints, nonconformances and CAPA, worked the same way every time.
 Standard workChangeovers, line clearance and shift handovers, held to the procedure.
 Safety and EHSPermits, lockout and incident reviews. The safety steps can’t be skipped.
 Engineering and supplier changeEvery change traced to the procedures, parts and suppliers it touches.
 Release and auditEvery record checked before a lot ships, with the audit trail already written.
See Vexum on your own procedures.
Tell us about your operation and our team will reply within one business day.